Pharmaceutical Machines
Effervescent Tablet Manufacturing Plant
We are a leading manufacturer and turnkey solution provider for Complete Effervescent Tablet Manufacturing Plants. We provide the entire range of machinery from granulation to tube packing under one roof, designed for moisture-controlled, GMP-compliant production. Our plant is engineered for low-humidity operation (below 25% RH), ensuring zero moisture absorption, high tablet stability, and fast disintegration.
Key Features
- Turnkey Solution - single-point responsibility from granulation to tube packing
- Dehumidified Environment Compatible for moisture-controlled production
- SS 316 Contact Parts for hygienic, GMP-compliant operation
- High Stability & Fast Dissolution with zero moisture absorption
- 100% Customizable as per Capacity
- Engineered for low-humidity operation (below 25% RH) ensuring zero moisture absorption, high tablet stability, and fast disintegration
- A complete solution for Pharma, Nutraceutical & Vitamin-C Effervescent Tablet manufacturing
Applications
Pharma Nutraceutical Vitamin-C Effervescent Tablets
Specifications
- Supply Scope: Turnkey line from granulation to tube packing
- Operating Humidity: Below 25% RH (low-humidity operation)
- Contact Parts: SS 316 construction
- Environment: Dehumidified environment compatible
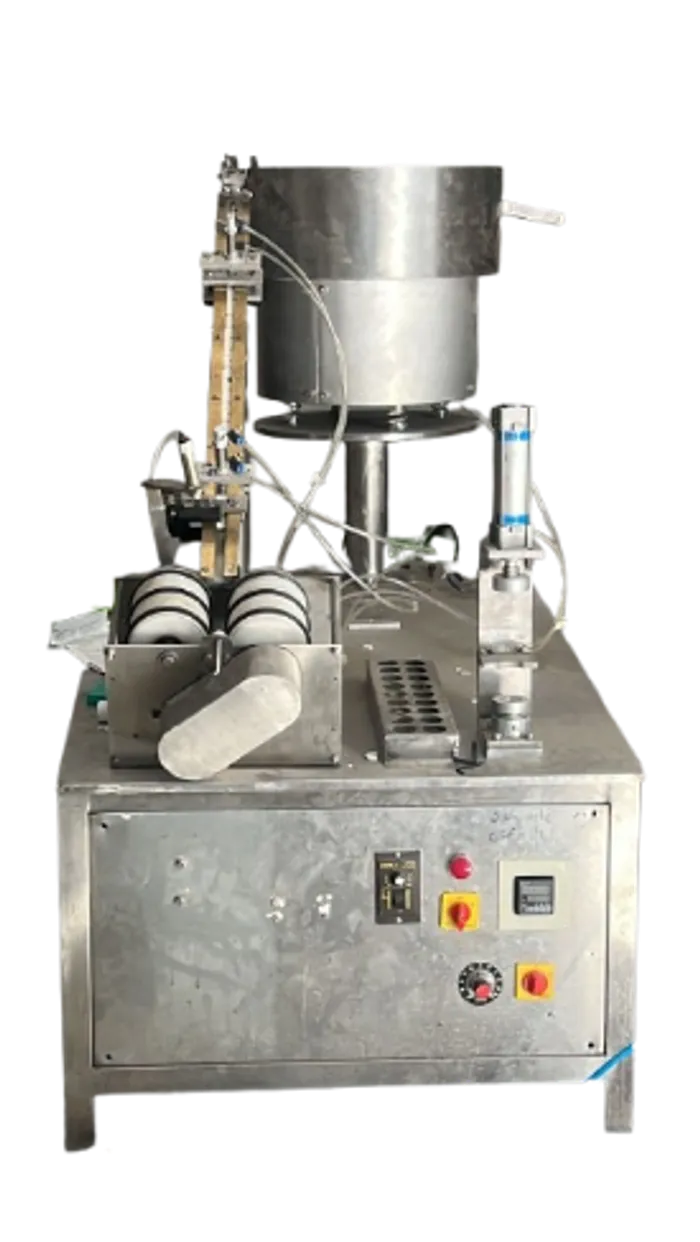
- Complete Line: Mixer / Blender, Tray Dryer, Vibro Sifter, Tablet Compression Machine, Tube Filling & Capping Machine, Tube Sticker Machine, Batch Coding & Stacking Conveyors
- Customization: 100% customizable as per capacity